
Release time:2026-09-22 10:34:02 view count:150
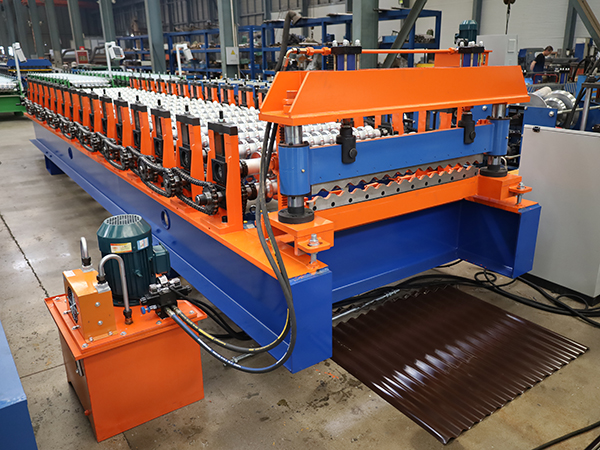
A cut to length machine, usually shortened to CTL, does the simple-sounding job of unrolling a coil, flattening it and chopping it into flat sheets. Anyone who has watched a badly specified line at work knows the job is not as simple as it sounds. Sheet that comes off a CTL line goes straight into presses, laser beds, roll formers or fabrication shops, and those downstream processes inherit every length error and every bit of residual curvature the line failed to remove. Blanking is where flatness and squareness are decided, and mistakes made here travel expensive.
Coil arrives with coil set, which is the memory of having been wound, along with possible crossbow and edge wave from the mill. Cutting first and hoping the sheet lies flat afterwards does not work. The leveller, with its staggered rolls bending the strip back and forth past its yield point, is what removes that shape. The number of leveller rolls and their diameter should be matched to the thickness range: a leveller built for thin material will not flatten heavy plate, and one built for plate will mark light sheet. Tell the manufacturer your full thickness range and let the leveller be sized from it.
The older approach uses a measuring wheel riding on the strip, feeding pulses to a counter. It is cheap and it works, but the wheel can slip, and it reads whatever surface it touches. The more accurate approach drives the strip through servo-controlled feed rolls and counts the roll rotation, so length is derived from a positive drive rather than from friction. If your customers hold you to a tolerance of a millimetre or less over several metres, servo feed is the honest answer. If you are blanking for rough fabrication, a well-maintained encoder wheel is fine and costs far less.
A stop-and-cut shear pauses the strip, cuts, then restarts. It is mechanically simple and perfectly adequate for modest volumes and thicker material. A flying shear accelerates the blade to strip speed, cuts on the move and lets the line run continuously, which is what makes high output possible on light gauge. The trade-off is cost and control complexity. Buy a flying shear because your volumes justify it, not because it appears modern; a stop-and-cut line running well beats a flying shear that is constantly out of adjustment.
Length accuracy is about measurement and feed. Squareness is about the shear itself: the blade must be square to the strip path and the strip must be held flat and centred at the moment of the cut. A line can hold length beautifully and still produce sheets whose diagonal measurements differ by several millimetres, which is enough to cause trouble in a press or on a laser bed. Check diagonals on the first sheets of every coil, not just length, and keep a record. Most squareness complaints trace back to blade clearance or to a strip guide that has drifted.
The decoiler sets the practical limits of the line. Coil inner diameter, outer diameter and weight all matter, and a machine whose mandrel will not take your supplier's coil ID is useless however good the shear is. Heavier coils mean fewer stops and better throughput, so the decoiler should be rated for the heaviest coil you intend to buy rather than the one you buy today. A coil car for loading is worth the money once coils exceed what a forklift can place safely, and it protects both the coil and the operator.
The exit end is where a lot of value gets quietly destroyed. Sheets dropped from height get dented edges; sheets slid across one another get scratched; sheets stacked without interleaving paper on pre-painted or polished material arrive looking second-hand. An automatic stacker with a controlled drop height and side squaring keeps the pile neat, which also makes it easier to band and to feed downstream. For coated material, ask about interleaving or protective film. It costs a little per tonne and prevents chargebacks that cost much more.
Slitting cuts a coil into narrow strips along its length; CTL cuts across it into sheets. Some operations need both, and combined slitting and cut-to-length lines exist for that reason. If your work is mostly producing blanks, buy a dedicated CTL and get the best leveller you can afford. A combined line makes sense when the product mix genuinely requires both, but it always involves compromise in the changeover and in the levelling capacity. Be clear about which operation dominates your output before the specification is fixed.
Provide coil width and thickness range, coil weight and ID, required sheet lengths and tolerances, material type, and target output per shift. Ask what the line does at your thinnest and thickest material rather than at a convenient average. Confirm blade material and the sharpening interval, and ask to see the line run your own coil during acceptance. A manufacturer that specifies against your real numbers is building a production tool; one that quotes a standard model number is selling you whatever is already in the workshop.
ASTM International. ASTM A1011/A1011M, Standard Specification for Steel, Sheet and Strip, Hot-Rolled, Carbon, Structural.
ASTM International. ASTM A568/A568M, Standard Specification for Steel, Sheet, Carbon, Structural, and High-Strength Low-Alloy, Hot-Rolled and Cold-Rolled.
International Electrotechnical Commission. IEC 60204-1, Safety of machinery - Electrical equipment of machines.
ISO. ISO 12100, Safety of machinery - General principles for design - Risk assessment and risk reduction.
Copyright © 2026-2027 Mingmu Roll Forming Machinery Manufacture All Rights Reserved